 Honeycomb
Select Welding Process & Diameters
Choose between Laser Welding or TIG Welding wire specifications.
0.15
mm
Spool / Rods0.2
mm
Spool / Rods0.3
mm
Spool / Rods0.4
mm
Spool / Rods0.5
mm
Spool / Rods0.6
mm
Spool / RodsCustom
Other Sizes
Contact Us →
0.8
mm
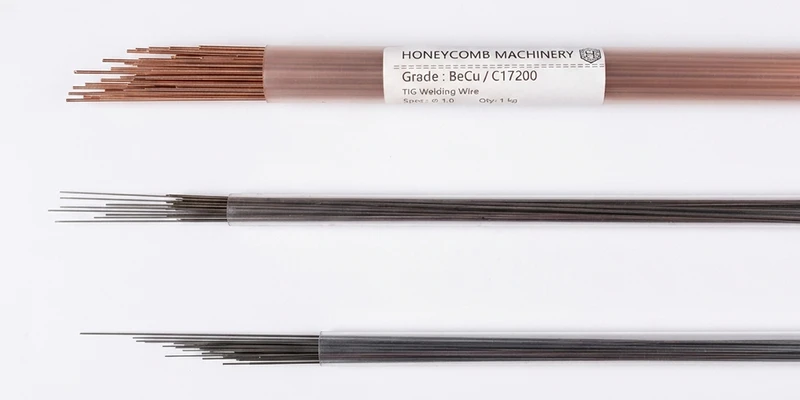
10 rods / tube1.0
mm
10 rods / tube1.2
mm
10 rods / tube1.6
mm
10 rods / tube2.0
mm
10 rods / tube2.4
mm
10 rods / tubeCustom
Other Sizes
Contact Us →
TECHNICAL DATA SHEET (TDS) & PROCESS GUIDE Standard: ASTM B196 C17200 / UNS C17500 (Beryllium Copper)
1. Chemical Composition (wt%)
| Element | Be | Co + Ni | Fe | Si | Cu |
|---|---|---|---|---|---|
| Specification | 1.80–2.00 | 0.20–0.60 | ≤ 0.15 | ≤ 0.15 | Balance |
2. Hardness & Welding Parameters
⚡ Laser Welding 0.15–0.6 mm
| Preheat Temp | Room Temp – 100°C |
| Pulse Power | 120–220 A |
| Shielding Gas | Argon ≥99.99% (4–6 L/min) |
| HAZ Impact | Extremely narrow HAZ, avoiding copper oxidation |
🔥 TIG Welding 0.8–2.4 mm
| Preheat Temp | 150°C – 200°C Recommended |
| Welding Current | 40–120 A (DCEN) |
| Shielding Gas | Argon ≥99.99% (8–12 L/min) |
| Post-Heat Relief | Slow natural cooling |
💡 Key Repair & Operation Instructions:
- Rapid Heat Dissipation: High copper content conducts heat extremely fast. Higher initial energy pulses may be needed during deposit compared to standard steel wires.
- Safety Notice: Ensure adequate local exhaust ventilation when grinding or arc-welding beryllium copper deposits.