 Honeycomb
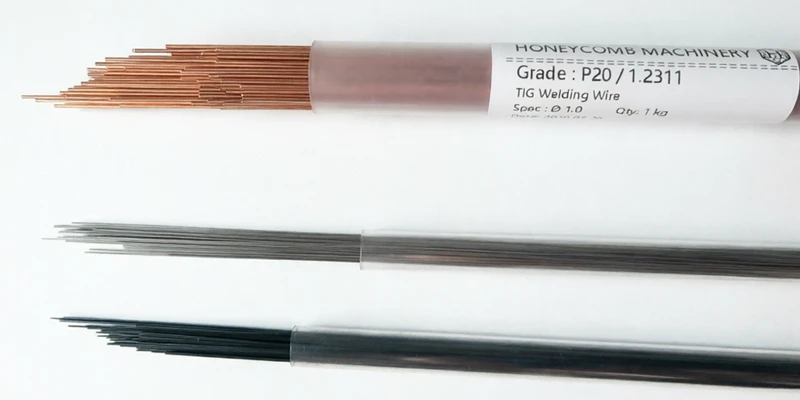
Select Welding Process & Diameters
Choose between Laser Welding or TIG Welding wire specifications.
0.15
mm
Spool / Rods0.2
mm
Spool / Rods0.3
mm
Spool / Rods0.4
mm
Spool / Rods0.5
mm
Spool / Rods0.6
mm
Spool / RodsCustom
Other Sizes
Contact Us →
0.8
mm
10 rods / tube1.0
mm
10 rods / tube1.2
mm
10 rods / tube1.6
mm
10 rods / tube2.0
mm
10 rods / tube2.4
mm
10 rods / tubeCustom
Other Sizes
Contact Us →
TECHNICAL DATA SHEET (TDS) & PROCESS GUIDE Standard: AISI P20 / DIN 1.2311 / GB 3Cr2Mo
1. Chemical Composition (wt%)
| Element | C | Si | Mn | Cr | Mo | Fe |
|---|---|---|---|---|---|---|
| Specification | 0.28–0.40 | 0.20–0.80 | 0.60–1.00 | 1.40–2.00 | 0.30–0.55 | Balance |
2. Hardness & Welding Parameters
⚡ Laser Welding 0.15–0.6 mm
| Preheat Temp | Room Temp – 100°C |
| Pulse Power | 90–180 A |
| Shielding Gas | Argon ≥99.99% (3–5 L/min) |
| HAZ Impact | Zero sink marks around micro-repair area |
🔥 TIG Welding 0.8–2.4 mm
| Preheat Temp | 150°C – 200°C Recommended |
| Welding Current | 35–100 A (DCEN) |
| Shielding Gas | Argon ≥99.99% (8–10 L/min) |
| Post-Heat Relief | Slow natural cooling |
💡 Key Repair & Operation Instructions:
- Matching Hardness: Deposited weld metal yields 30–34 HRC, perfectly matching pre-hardened P20 parent steel to eliminate boundary haloing during EDM and polishing.
- Parting Line Repair: Use short arc pulses to tightly control heat input, avoiding undercut or sink marks on precision parting surfaces.