 Honeycomb
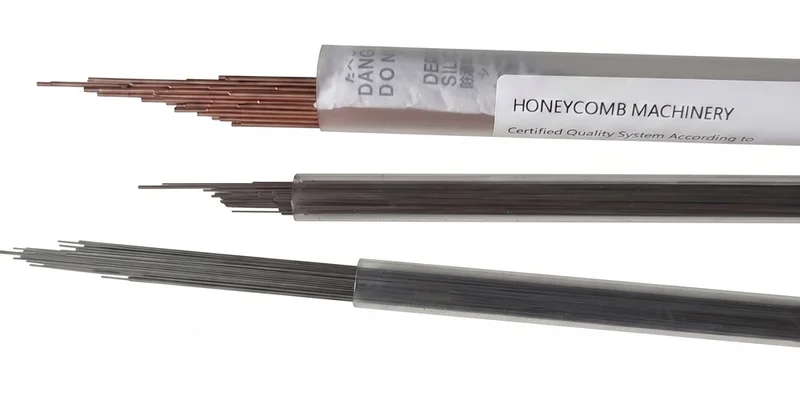
Select Welding Process & Diameters
Choose between Laser Welding or TIG Welding wire specifications.
0.2
mm
Spool / Rods0.3
mm
Spool / Rods0.4
mm
Spool / Rods0.5
mm
Spool / Rods0.6
mm
Spool / RodsCustom
Other Sizes
Contact Us →
0.8
mm
10 rods / tube1.0
mm
10 rods / tube1.2
mm
10 rods / tube1.6
mm
10 rods / tube2.0
mm
10 rods / tube2.4
mm
10 rods / tubeCustom
Other Sizes
Contact Us →
TECHNICAL DATA SHEET (TDS) & PROCESS GUIDE Standard: Special SKD11-3 Filler Metal / High-Toughness Modification
1. Chemical Composition (wt%)
| Element | C | Si | Mn | Cr | Mo | V | Fe |
|---|---|---|---|---|---|---|---|
| Specification | 0.70–0.90 | 0.30–0.60 | 0.30–0.60 | 9.00–11.00 | 1.20–1.60 | 0.20–0.50 | Balance |
2. Welding Parameters: Laser vs. TIG
⚡ Laser Welding 0.2–0.6 mm
| Preheat Temp | Room Temp – 100°C |
| Pulse Current | 110–210 A (Laser Power: 200–400 W) |
| Shielding Gas | Argon ≥99.99% (3–6 L/min) |
| HAZ Impact | Minimal HAZ, preventing punch edge chipping |
🔥 TIG Welding 0.8–2.4 mm
| Preheat Temp | 300°C – 400°C Mandatory |
| Welding Current | 40–160 A (DCEN) (Precision Repair Standard) |
| Shielding Gas | Argon ≥99.99% (8–12 L/min) |
| Post-Heat | Slow cooling or 500°C stress relief annealing |
💡 Key Repair & Operation Instructions:
- Enhanced Toughness & Anti-Chipping: Compared with standard SKD11, SKD11-3 reduces carbon content to moderate levels while boosting Mo-Cr toughness, preventing weld line spalling under severe impact loading.
- Ideal Buffer / Buildup Layer: Can be used as a tough buffer layer before surfacing with extremely hard cutting alloys.